If you’re in the plastics manufacturing game, you’ve probably heard the term “shot weight” thrown around more than a hot runner nozzle at a mold shop. And if you’re my customer—someone who’s weighing every dollar spent on equipment that makes or breaks their daily output—you’ve probably stared at an electric pre-plasticizing injection molding machine spec sheet and thought, “Wait, what does that number actually mean, and why does it matter more than the machine’s brand name?” Let’s break this down like we’re chatting over a coffee after a long day on the floor, no stuffy engineering jargon (okay, maybe a tiny bit, but I’ll keep it simple). Electric Pre-Plasticizing Injection Moulding Machine

First, let’s get one thing straight: shot weight isn’t just a random number manufacturers pull out of thin air. It’s the maximum amount of plastic resin your machine can inject into a mold in one single shot—think of it like a espresso machine’s shot volume, but way bigger and way less caffeinated. But here’s the big difference with electric pre-plasticizing machines vs. old hydraulic ones: pre-plasticizing is a game-changer here. These machines have two separate stages: one that melts the resin (the pre-plasticizing unit, usually a separate screw or chamber) and one that injects it into the mold. That means the shot weight isn’t tied directly to the injection unit’s size like it is on basic models. I sell these machines, so let me tell you—this is one of the first questions new buyers ask, and it’s also the one that messes up their production if they get it wrong.
Let’s use a real example. Last month, a customer from Detroit reached out because they were using a hydraulic machine that could do a 500-gram shot, but they were switching to our electric pre-plasticizing models to save energy. They told me they needed a 450-gram shot for their automotive door handles. I had to stop them right there—“Wait, that’s not how you measure shot weight for pre-plasticizing machines.” Because with a standard electric machine (no pre-plasticizing), the shot weight is just the capacity of the injection screw barrel. But pre-plasticizing? The pre-plasticizing unit melts the resin first, then transfers it to the injection unit. So the shot weight depends on two things: the volume of the injection barrel (the final amount you can push into the mold) and the density of your resin.
Oh right, density! That’s the secret sauce most people miss. If you’re using ABS plastic, which has a density of around 1.05 g/cm³, a 1000 cm³ injection barrel will give you about 1050 grams of shot weight. But if you’re working with polypropylene (PP), which is lighter at 0.91 g/cm³, that same 1000 cm³ barrel only gives you ~910 grams. I see buyers mess this up all the time—they grab a spec sheet that says “max shot weight 1000g” assuming that’s always true, but if they switch resins, that number changes. That’s why when you talk to me, I always ask what resin they’re using, not just what part size they’re making.
Another big point: effective vs. theoretical shot weight. Theoretical is just the math of the barrel volume times resin density—simple, right? But effective shot weight is what you actually use on the shop floor. Why? Because you can’t inject every last bit of melted plastic out of the barrel; there’s always a small leftover (called the “dead volume”) that stays in the screw tip. For our electric pre-plasticizing machines, that dead volume is way smaller than hydraulic ones—usually 1-2% of the total shot, vs. 3-5% for hydraulics. That’s a huge win because it means you’re wasting less resin per shot, which adds up when you’re running 24/7. The Detroit customer I mentioned earlier? They were using a hydraulic machine that left 25 grams of plastic in the barrel every shot, so their effective shot was only 475 grams. With our pre-plasticizing model, the dead volume is 5 grams, so their 450-gram actual part fits perfectly without wasting material.
Wait, also—shot weight isn’t just about the part size. You have to account for the gating system too, right? That’s the runners and gates that feed plastic into your mold, which are extra grams of resin. If your door handle part is 450 grams, the gating system might add another 50 grams, so your total shot weight needs to be 500 grams, not 450. I can’t tell you how many times a buyer calls me panicking because their mold is making a 450g part, but their machine can only do 440g—they forgot the gating! That’s where our sales team’s trick comes in: we always ask for part CAD files, or at least the part’s dimensions, so we can calculate the total shot weight including runners before they even buy the machine.
Now, let’s talk about why electric pre-plasticizing machines have a leg up here. Traditional electric machines (without pre-plasticizing) do everything in one unit: they melt the resin and inject it at the same time. That means the screw size is the only limit on shot weight, and changing shot weight requires swapping out the entire screw barrel—something that takes hours, not minutes. Pre-plasticizing machines? The pre-plasticizing unit is separate, so you can adjust shot weight by changing the amount of melted resin transferred to the injection unit, not swapping parts. That’s a game-changer for small to medium runs, or manufacturers who make multiple part sizes. I had a customer in Texas who makes plastic packaging for food—they run 10 different part sizes a week, from small lids to bigger containers. With our electric pre-plasticizing machines, they can switch shot weight from 50g to 300g in 10 minutes, vs. 2 hours with their old electric machine. That saved them over $10k a year in downtime.
But here’s the catch: you can’t just go for the maximum shot weight listed on the spec sheet and call it a day. I see buyers do that all the time—they think a machine with a 1000g max shot is better than a 800g one, but if their actual shot is only 500g, they’re overspending on a machine they don’t need. Not only that, but running a machine at 70-80% of its max shot weight is the sweet spot for efficiency. If you run it at 100% max, you’re putting more stress on the screw and barrel, leading to more wear, more downtime, and higher maintenance costs. If you run it at less than 50%, you’re wasting energy on heating extra resin that you don’t need, and your cycle times might be slower. So when a buyer tells me they need a 500g shot, I recommend a machine with a max shot of 600-700g, not a 1000g one. That’s the sweet spot.
Also, let’s not forget about process control, which is huge with electric pre-plasticizing machines. The pre-plasticizing unit lets you control the melt temperature, melt pressure, and plasticization rate separately from the injection unit. That means you can get a more consistent shot weight, even when you’re running different resins. For example, if you switch from PP to PET, the pre-plasticizing unit can adjust the melt temperature without messing with the injection pressure, so your shot weight stays consistent, and your parts have fewer defects. I had a customer in Ohio who was getting 15% defect rates with their old hydraulic machine because shot weight was inconsistent when switching resins. With our pre-plasticizing model, their defect rates dropped to 2%, and they saved $20k a year in scrap.
Wait, I should also clear up a common myth: shot weight vs. shot volume. A lot of people mix these up. Shot weight is grams (or ounces) of resin, shot volume is cubic centimeters (cm³) or cubic inches (in³). We always give both numbers in our spec sheets, because depending on your resin, you’ll need one or the other. For example, if you’re working with a high-density resin like HDPE, shot weight is more important, but if you’re working with a low-density resin like EVA, shot volume is a better measure. Our team will walk you through that—no confusing numbers, just what you actually need for your process.
Let me circle back to why this matters for you, the buyer. If you’re choosing between a hydraulic, standard electric, or electric pre-plasticizing machine, shot weight is one of the top factors (along with energy costs, cycle times, and maintenance). Electric pre-plasticizing machines are more expensive upfront, but the precision in shot weight, lower waste, and higher efficiency add up to big savings over time. I’ve had customers tell me they made back the extra cost of our machines in 18 months, just from less scrap and lower energy bills.
But here’s the thing—every job is different. What works for the Detroit automotive customer doesn’t work for the Texas packaging customer, and vice versa. That’s why when you reach out to me, I don’t just push the biggest machine I have. I ask questions: What resin do you use? What’s your part size, including runners? How many shots do you run per day? Do you switch part sizes often? What’s your defect rate now? All of that goes into figuring out the right shot weight capacity for your machine.
If you’re still confused about shot weight, or you’re trying to figure out which electric pre-plasticizing injection molding machine is right for your business, don’t guess. That’s a quick way to end up with a machine that’s either too big (wasting money) or too small (not meeting production needs). I’ve been in this game for years, selling these machines, and I’ve seen almost every mistake a buyer can make with shot weight. Let me help you avoid them.
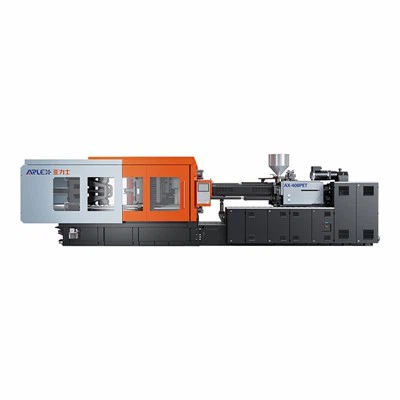
At the end of the day, shot weight isn’t just a spec number—it’s the difference between a production line that runs smoothly, wastes almost no material, and makes consistent parts, and one that’s always breaking down, throwing away resin, and missing deadlines. If you’re ready to upgrade your molding process with an electric pre-plasticizing machine, or you just want to talk through your current shot weight needs, get in touch with our team. We’ll give you straight answers, no sales fluff, and help you find the machine that fits your exact requirements.
Temperature Control Unit References
Rosato, D. V., & Rosato, M. G. (2000). Injection Molding Handbook (3rd ed.). Kluwer Academic Publishers.
Groover, M. P. (2007). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (3rd ed.). John Wiley & Sons.
plastics molding equipment guide: Shot weight calculation for pre-plasticizing machines. Industrial Plastics Journal, 2022.
Ningbo Yalishi (Arlex) Plastic Machinery Co., Ltd.
Address: No.63, Huangsu East Road, Industrial Zone, Dongqian Lake Tourist Resort, Ningbo, Zhejiang Province
E-mail: leo@arlex.cn
WebSite: https://www.arleximm.com/
